Why we organise by job
Nobody buys a rotary valve. They buy a way to get flour out of a silo without losing air pressure.
Equipment catalogues are organised by machine, because that is how machines are built and sold. Plants are organised by job, because that is how problems arrive. Somebody has to unload a tanker, feed a press, keep a baghouse from blinding or stop dust escaping at a transfer point.
This section follows the second order. Each page names a job, in a named industry, and works from the duty to the equipment.
The jobs on this site
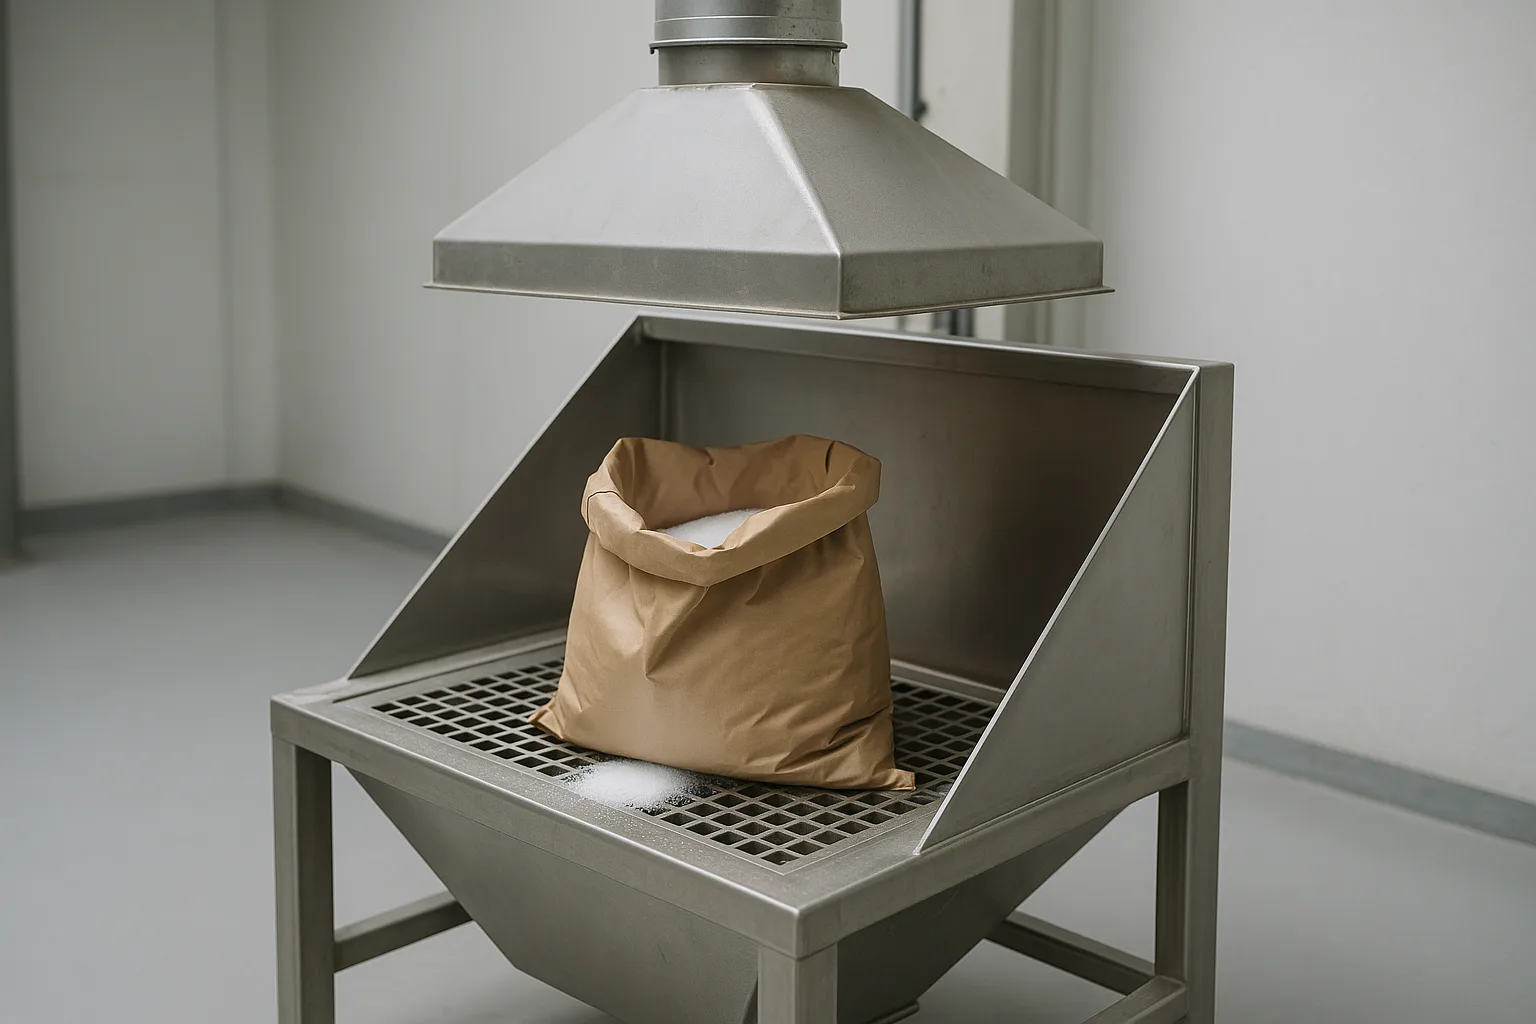
- Receiving: tanker unloading, bulk bag discharge, sack tipping, drum emptying.
- Storage and reclaim: silo discharge, bin activation, flow aids, level and inventory.
- Transfer: pneumatic conveying in dilute and dense phase, mechanical conveying, routing to several destinations.
- Dosing and preparation: gravimetric and volumetric feeding, batching, screening, mixing, milling.
- Protection: dust collection, explosion venting and isolation, containment for potent compounds.
- Despatch: bagging, big bag filling, truck and ship loading.
What makes a job difficult
The duty is rarely constant
A conveying line sized for the average rate fails at the peak. A feeder sized for the nominal recipe cannot hold tolerance at the smallest addition. The first question on any application page is therefore the range, not the figure: the lowest rate, the highest rate, and how often each occurs.
The machines interact
Most jobs need a chain, and the weakest link decides the result. A vacuum receiver that cannot clean its filter will starve the feeder below it, whatever the feeder is capable of. A silo that bridges makes the discharge equipment irrelevant.
Where a page recommends equipment, it names the interface as well: what has to be true upstream and downstream for the machine to perform as specified.
The industry changes the answer
The same job has different constraints in different industries. Bulk bag discharge in a food plant has to be cleanable and allergen-segregated. In a cement works, the same job is about wear and dust. In pharmaceuticals, it is about containment and validation.
That is why the pages are written by job and industry together, rather than by job alone.
How to use this section
If you know the job, start here and follow the links into the technologies it uses. If you know the material, start from the material pages and arrive at the same place from the other side. If you know the machine, the technology pages are the way in.
Every application page carries the same structure: the problem as operators describe it, the result a good design delivers, how the job is normally arranged, the factors that decide the selection, and the failure modes that show up when one of them was missed.
What these pages do not do
They do not size equipment. Sizing needs measured material properties, the real duty cycle and the plant layout, and it belongs with the supplier who will stand behind the result.
What they do is shorten the distance between a problem and the right question. Most bad installations are not bad machines; they are machines selected against the wrong duty, or installed without the condition that made them work in the reference plant.
How the duty is written down
Most arguments between a plant and a supplier come from a duty that was never written down properly. Five lines prevent them.
- Material and condition: name, supplier, particle size distribution, moisture range, temperature at the inlet.
- Rate: average, peak, and the duration of the peak. A line that runs ten minutes at double rate is a different line.
- Geometry: horizontal distance, vertical lift, number and radius of bends, the position of every destination.
- Environment: area classification, hygiene standard, washdown, ambient temperature and humidity.
- Acceptance: what will be measured on handover, and against which tolerance.
Where the limits sit
Conveying velocity
Dilute phase conveying carries material suspended in air and needs a velocity above the saltation point, which for most powders puts it in the range of roughly fifteen to thirty metres per second. Dense phase moves material as slugs at a fraction of that, typically single digits.
The difference is not a preference. High velocity breaks fragile product and erodes bends; low velocity needs more pressure and a vessel rather than a blower. Fragile or abrasive material pushes the choice towards dense phase, long distances and high rates towards dilute.
Feeding accuracy
A volumetric feeder meters a volume and assumes a density. A gravimetric feeder weighs, and therefore holds tolerance when the density changes. Wherever the recipe tolerance is tighter than the density variation of the material, the question is already answered.
Dust capture
Capture happens at the source or it does not happen. Extraction volume follows the open area and the face velocity needed to hold dust in, not the size of the machine, and a hood that is too far away cannot be fixed with a bigger fan.
The failure modes that repeat
Across every job on this site, the same four causes account for most of what goes wrong after commissioning.
- Sized for the average. The peak rate was known and left out of the specification, so the line runs at its limit every shift.
- The interface was nobody's scope. Two suppliers each delivered correctly, and the connection between them was designed by neither.
- The material changed. A new supplier, a finer grade or a wetter season moved a property that the design depended on.
- Cleaning was an afterthought. The equipment performs and cannot be cleaned in the time the plant has, so it is opened less often than it should be.
None of these is exotic, and all four are cheap to prevent at the specification stage and expensive to fix afterwards. Each application page names the ones that apply to that job.