
Application
Valve and Airlock Selection for Mining and Mineral Plants
Answer in brief
In mineral plants a valve is a consumable with a service life measured in months.
The design question is not whether it will wear but whether the wear is confined to parts that were meant to take it, and whether those parts can be changed without cutting the plant open.
- Put the wear where you can reach it.
- Size for the largest particle, not the average.
- Have the spare on the shelf before the first failure.
Reviewed October 21, 2026
The problem
Abrasive minerals destroy valves, and they do it predictably. Silica sand, alumina, iron ore fines and crushed aggregate erode seats, blades and rotor tips within months, and the first symptom is not failure but leakage: a gate that no longer seals, a rotary valve whose clearance has grown until half the conveying air goes the wrong way.
The forces are also larger than catalogue selection suggests. A knife gate under a loaded bin has to cut through a column of material, not swing in clear air, and a blade selected on nominal capacity bends on the first full bin.
Oversize is the other recurring fault. A screen that passes a tramp particle, a lump that formed in a damp bin, or a bolt from upstream maintenance jams a blade that handled the nominal product without trouble, and the jam is what breaks the actuator.
Desired outcome
A valve whose wear life is known rather than discovered, with wear concentrated in replaceable liners, blades and rotor tips, and with access that lets a change happen in a planned shutdown instead of an unplanned one.
A clearance or seal condition that is measured as a performance indicator, so the plant knows the valve is leaking before the conveying system tells it the hard way.
The same duty in a pet food plant is governed by fat on the seal face and by changeover count per shift, not by abrasion, and a hard-faced blade helps nothing there.
Process approach
Selection starts with the particle size distribution including the top size, and with the honest version of it: what the screen passes when it is worn, not what it passes when it is new.
For bins and chutes, knife and roller gates with replaceable liners are the normal answer, specified with the blade treated as a scheduled change rather than a failure. Where the blade has to cut through material under a head, the actuator and the frame are sized for that, not for the free swinging case.
Where the valve is a pressure boundary, a rotary valve with a hardened or tipped rotor in a lined housing is used, and the tip clearance is logged. Clearance growth is the measurable form of wear, and a trend line gives weeks of warning.
Diverter valves in abrasive service wear at the junction, not at the actuator, so the liner at the point where the stream changes direction sets the interval. A diverter chosen for its actuator and lined as an afterthought wears through at the one place nobody specified.
- Top size and worn screen output used for sizing, not the nominal distribution.
- Wear concentrated in liners, blades and tips that are listed as consumables.
- Gate actuators and frames sized for cutting through a loaded column.
- Rotor tip clearance logged as a performance indicator with a trend.
- Diverter liners specified at the junction, which is where the stream turns.
- Spares held locally, with the change procedure written before it is needed.
Selection factors
- Abrasiveness and particle angularity, which decide liner material: hardened steel, ceramic tile, or a replaceable rubber depending on impact angle.
- Top particle size and credible tramp material, which decide the opening and the jam case.
- Head of material above a gate, which decides the closing force and the frame.
- Service access, because a valve that needs the chute cut to change a blade will be run past its life.
- Moisture content, since damp mineral builds up and turns a sliding surface into a sticking one.
- Pressure duty, which decides whether the valve has to seal at all or only has to stop flow.
Common failure modes
- Blade sized on nominal capacity and bent by the first full bin
- Wear spread across the housing instead of into replaceable liners, so the whole valve is the spare
- Oversize particle jamming a gate and destroying the actuator that was never specified for it
- Rotor clearance never measured, so leakage is discovered through conveying performance
- Diverter lined everywhere except the junction where the stream actually turns
- No spare on site, so a scheduled consumable becomes an unscheduled outage
Partner with powderbulkvideos.com
Put a relevant technical solution in this decision path.
Connect your company and video evidence with clearly labelled visibility where engineers evaluate this material, application, industry or product.
Frequently asked questions
How long should a valve last in abrasive service?
Months rather than years, and the number matters less than knowing it. A measured wear rate turns a valve into a scheduled consumable; an unmeasured one turns it into an unplanned stop.
What is the best indicator that a rotary valve is worn?
Rotor tip clearance. It grows steadily and it can be measured in a shutdown, so a simple log gives weeks of warning before leakage starts affecting the conveying system.
Where do diverter valves wear first?
At the junction, where the stream changes direction and the particles strike the wall. The actuator usually outlives several liners, so the liner specification at that point sets the service interval.
Related content
Continue exploring
Move from this page to the companies, videos and technical topics that add useful context.
Companies
Videos
Coperion
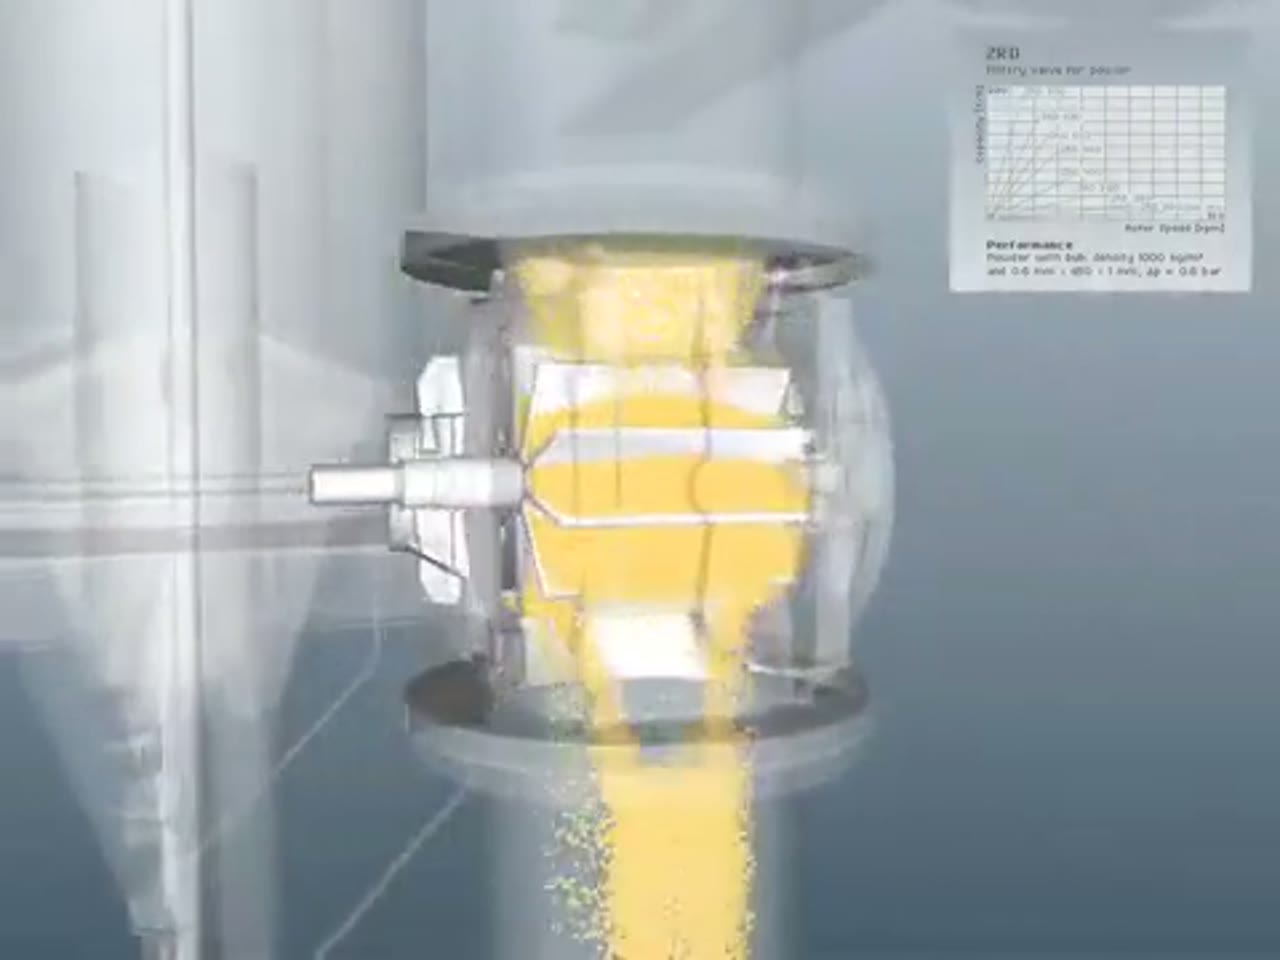
Coperion ZRD Rotary Valve for Powder Applications
Coperion presents the ZRD rotary valve and the design choices that adapt it to powder discharge, metering and pneumatic-conveying service.
Total reach: 10,524

Kice Industries
Kice VJX Airlock Installation
Kice Industries demonstrates installation considerations for its VJX airlock at a dry-bulk process interface.

Vortex – Solids & Bulk Handling Components
Vortex®: Orifice Slide Gate Valve
Vortex's video presents the Orifice Slide Gate Valve: a linear blade carries a machined orifice that moves into or out of alignment with the process connection to isolate or regulate dry-bulk flow.
Total reach: 68,292